Article Snapshot
What this article covers
A finish description must connect appearance, coating identity and functional interfaces. This guide explains how buyers and engineers can define reproducible cosmetic acceptance while keeping performance qualification, process evidence and rework decisions explicit.
- Identify the complete finish system and the surfaces where each requirement applies.
- Agree viewing conditions and controlled boundary samples before production.
- Protect masked, contact and threaded features through finishing and repair.
- Separate cosmetic inspection from performance testing and receiving disposition.
A TV metal back plate can match an agreed color and still create an assembly problem. Coating may enter a threaded feature, cover an intended contact area or change the seating of a mating component. Conversely, a visible mark may be unacceptable to one inspector and acceptable to another because they examine different surfaces under different lighting. A usable finish specification connects these decisions before a disputed shipment makes them urgent.
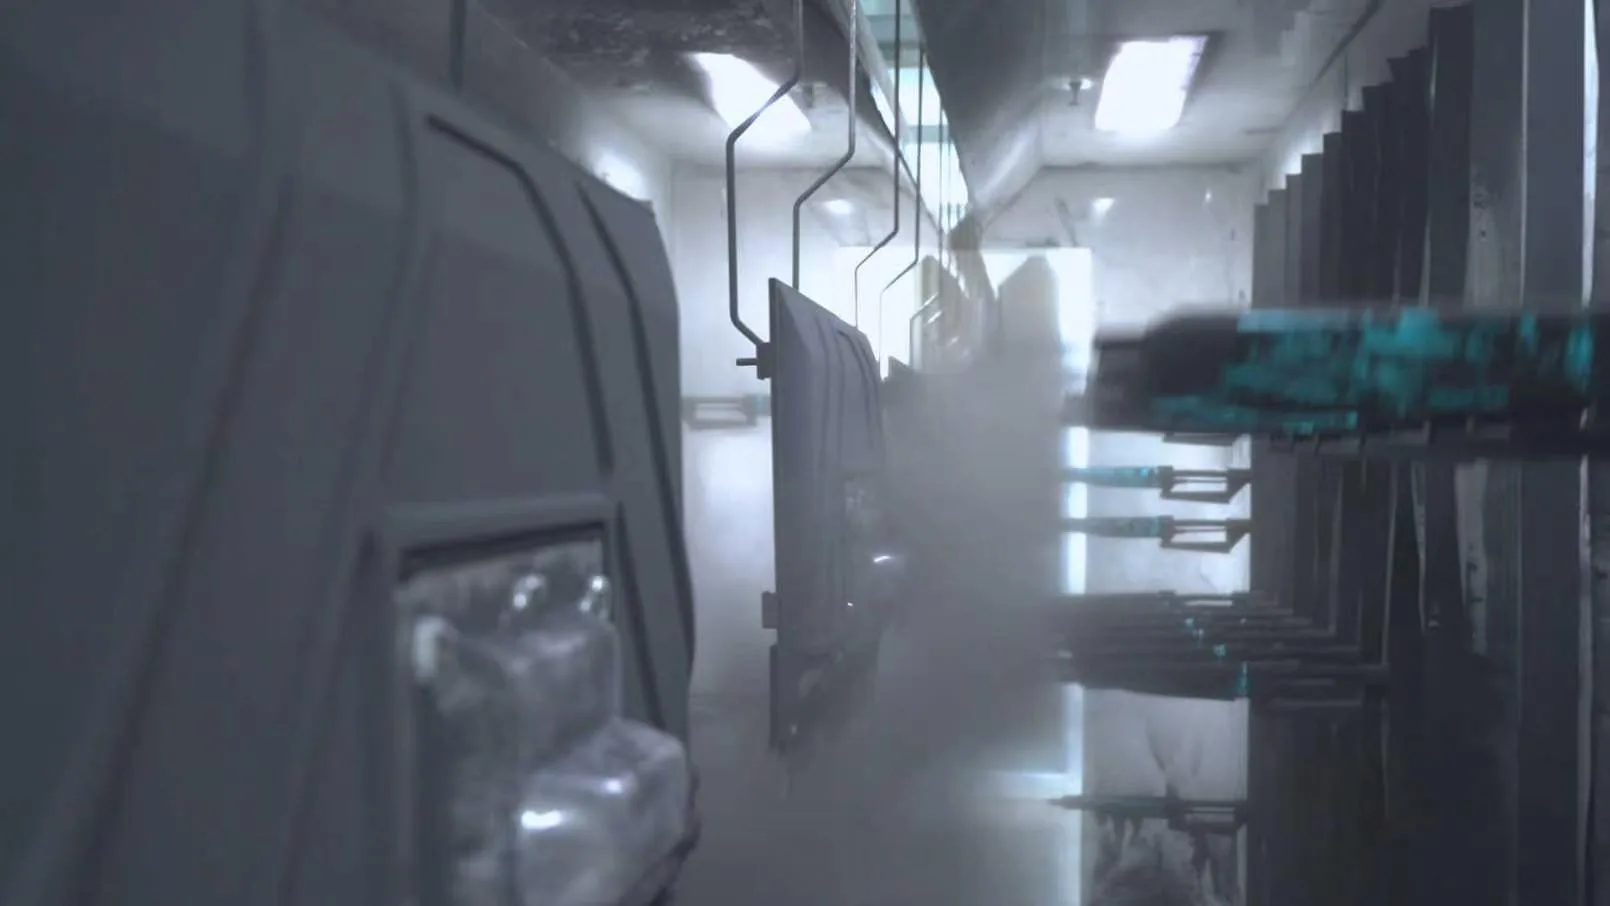
This guide focuses on defining and accepting the finished surface. The supplied coating workshop photograph above shows hanging panels in a manufacturing setting; it does not establish the chemistry, film thickness, cure condition or performance of a specific tested finish. Project conclusions require the actual part specification and evidence linked to that part.
1. Define the finish as a controlled system
Start with the part number, drawing revision and finish-specification revision. Identify whether the order calls for the sheet's existing metallic surface, an additional organic coating or a specified multilayer system. Terms such as “black finish,” “painted” and “same as sample” leave too much unresolved unless the approved documents explain their scope and authority.
For an additional coating, request the approved product or system identification, applicable substrate, pretreatment route, color reference, texture, gloss requirement and specified film-thickness locations. Record which items the customer controls and which the finisher proposes for approval. A change in coating supplier or formulation should enter that review process even when the commercial color name remains unchanged.
Distinguish acceptance requirements from process settings. The customer may define a finished thickness range and performance requirement while the coating supplier provides the application and curing instructions needed for its product. Keep those records connected without inventing a generic oven setting for every plate. Identify who can approve alternatives and which evidence is needed before an alternative becomes the production baseline.
2. Map cosmetic and functional surface zones
Mark the actual part drawing or a controlled surface map. Identify surfaces visible in the delivered TV, surfaces exposed during assembly or servicing, and concealed regions. The intended product and handling context determine the classification. An internally mounted plate and a plate visible through rear openings may need different appearance definitions even when their manufacturing route is similar.
For each zone, describe relevant defect types: scratches, dents, contamination, inconsistent texture, color variation, coating runs or local lack of coverage. State whether the decision concerns appearance, protection, assembly or several of these. A concealed location does not automatically permit exposed substrate or loose coating; its functional requirements still need a disposition.
General planning example: this surface map prompts project decisions and supplies no universal defect limits.
| Surface region | Decision to define | Reference evidence | Responsible reviewer |
|---|---|---|---|
| Visible rear-facing region | Appearance under agreed viewing conditions | Zone map and cosmetic boundary samples | Customer appearance owner |
| Concealed formed region | Coverage and permitted handling marks | Finish specification and defect examples | Customer quality engineer |
| Mating or seating surface | Coating presence and finished interface condition | Assembly detail and fit evidence | Mechanical design owner |
| Specified contact or threaded feature | Mask boundary and functional verification | Feature detail and applicable test plan | Design and manufacturing reviewers |
3. Make cosmetic viewing conditions reproducible
“No visible defects” becomes useful only after the team defines how the surface is viewed. Agree the lighting source and arrangement, background, observation distance, viewing angle, examination time and part orientation. Define whether inspection uses normal vision, corrective lenses or specified magnification. These are project choices; an inspector should not introduce a flashlight or extreme grazing angle during receiving without an agreed reason.
Include the part's inspection state. Identify whether it is loose or assembled, whether a temporary protective film has been removed, and what approved cleaning is permitted before assessment. A cleaning step that changes the coating cannot be treated as neutral preparation. Provide a safe handling location so the inspection itself does not introduce fingerprints or contact marks.
Instrumental gloss and visual appearance answer related but different questions. ISO 2813:2014 describes gloss determination using 20°, 60° and 85° geometries. If the project specifies gloss measurement, agree the applicable geometry, locations and limits. A gloss value alone does not resolve scratches, texture differences or overall cosmetic approval. Color measurement likewise needs its own agreed method and comparison conditions when required.
4. Approve boundary samples with a defined purpose
A target sample communicates the desired appearance; a boundary sample communicates the edge of an agreed decision. Identify whether each sample represents acceptable color variation, a permitted local mark, an unacceptable scratch or another specific condition. Avoid one unsigned “golden sample” becoming an assumed answer to every question about the part.
Label each reference with its part revision, finish revision, sample identifier, represented characteristic, surface zone, approval date and approving parties. Record the viewing conditions used for approval. Retain equivalent references at the locations that make acceptance decisions, and establish how disagreements between those references are resolved. Photographs can locate a mark, but uncontrolled screens and lighting make them weak substitutes for physical appearance references.
Protect reference samples from wear, contamination and unnecessary handling. Agree a review or replacement process when their condition changes. A sample is evidence only within its recorded role: an acceptable texture patch does not authorize a coating substitution, and a cosmetic rejection sample does not define adhesion performance. Keep numerical requirements controlling where the specification assigns them authority.
5. Confirm substrate and coating compatibility
The starting surface matters to the finishing route. Supply the finisher with the actual substrate and existing surface-treatment information, including relevant oils or treatments from upstream operations. A material designation alone may leave those details unresolved. Ask how cleaning, pretreatment and the selected coating are intended to work together on the delivered surface.
GalvInfoNote 2.12, Pretreatments for Metallic-Coated Sheet, explains that factory-paint pretreatments are distinct from treatments used for other purposes and discusses their role in coating adhesion. Its background supports asking about the actual incoming surface and selected pretreatment. It does not identify the process used in the photograph or prescribe a KINGSUN production recipe.
Review compatibility using the coating supplier's current technical information and project-specific trial evidence. Identify whether trials represent the formed production part or only a flat coupon, especially around bends, edges and recessed areas. Reassess when the incoming treatment, cleaning route or coating system changes. Keep detailed base-material selection in the SGCC material guide; the finish decision here concerns the compatibility of the approved combination.
6. Define masking, contact areas and threaded features
Use feature-level drawing details wherever coating presence changes function. Identify intended uncoated zones, permitted transition boundaries, edge coverage requirements and allowed rack-contact locations. A broad instruction to “mask contact points” is incomplete if the production team cannot locate them or understand the permitted overspray boundary.
Where the design includes an electrical contact, the responsible designer must define the required interface and verification. Surface appearance alone cannot establish electrical suitability. Similarly, a thread that looks open may still require an agreed gauge or assembly check after finishing. Define the finished condition needed for studs, holes and mating seats rather than assuming that every dimension applies before coating.
Review the proposed hanging or supporting method with these zones in mind. Contact marks may be permissible in an approved location but unacceptable elsewhere. Record whether masking removal, thread cleaning or another secondary operation is permitted, and how it will be checked. Uncontrolled scraping after coating can alter adjacent surfaces, so include such operations in the process review instead of leaving them to an assembler's judgment.
7. Keep performance qualification separate from cosmetics
A visually approved sample establishes only its agreed cosmetic role. Performance requirements need a separate plan identifying the property, method and edition, specimen, preparation, conditioning, acceptance criterion, frequency and report owner. Depending on the application, the plan may address coating thickness, adhesion-related behavior, resistance to specified exposure or a functional interface. Select applicable tests through engineering review.
ASTM D3359-23 covers tape-test rating of relatively ductile coating films on metallic substrates and identifies limits to the distinctions it can make. ISO 2409:2020 assesses resistance to separation after a lattice cut; its public abstract explicitly distinguishes that assessment from measuring adhesion. The methods should not be silently substituted or their classifications treated as interchangeable.
Confirm suitability for the actual coating, thickness and texture before selecting a method. Agree whether destructive checks use production parts or representative specimens and how those specimens link to the lot. An exposure-test result must retain its conditions and assessed endpoints; a stated salt-spray duration cannot by itself establish TV service life. Cosmetic inspection and performance reports should both reach a disposition when both are specified.
8. Resolve a sample dispute against the agreed baseline
Hypothetical sample-dispute example: a buyer rejects a faint scuff on a rear-facing coated region after viewing it with a handheld light at a shallow angle. The supplier accepted the same region under the approved inspection arrangement. The retained target sample shows the intended color and texture, but neither team has approved a scuff boundary sample. This is a fictional planning scenario, not a KINGSUN customer result.
First preserve the disputed part and its identity. Compare the approved surface-zone map, viewing instruction and existing sample approvals. Repeat the examination under the agreed conditions and record the observation without cleaning or polishing away the evidence. If the scuff is outside an existing criterion, follow that disposition; if the criterion is incomplete, route the missing decision to the authorized appearance owner.
A decision for this lot should state its quantity, location and conditions. If the teams approve a new boundary reference, issue it through the controlled specification process and identify its application to future lots. Do not quietly convert a one-time concession into a permanent standard. Any concern about coating continuity or function needs its own review even if the appearance dispute is settled.
9. Decide what repaired surfaces must demonstrate
Agree whether local touch-up, stripping and recoating, or other repair routes are permitted before using them on deliverable parts. Define eligible defects and locations, the authorized process and the evidence required afterward. A repair that makes a mark less visible may still change texture, film build or the condition of a neighboring interface.
Use a separate rework approval when the normal process evidence does not cover the proposed route. Ask whether additional preparation or heating affects the substrate, geometry, threads or previously finished features. Decide which original checks remain valid and which must be repeated. A cosmetic comparison alone should not close a repair whose coating integrity or assembly condition is unresolved.
Retain the original lot identity and identify repaired quantities so receiving can connect them to the approved disposition. Where repair is unsuitable, segregate the affected parts and record the replacement or scrap decision. Repair limits should come from the actual system and customer agreement; neither a universal number of recoating cycles nor an assumed permission to touch up every hidden region is appropriate.
10. Give receiving a complete acceptance decision
Receiving needs a current, usable instruction set rather than the history of the finish discussion. Provide the drawing and finish revisions, surface map, viewing conditions, sample register, applicable test evidence and any authorized deviations. Identify the lot and the sampling or inspection plan agreed for that order. A supplier photograph is supporting context, not automatic evidence that the delivered lot matches every requirement.
General planning example: keep these decisions separate in the receiving record so a pass in one category cannot hide an unresolved category.
| Acceptance category | Check against | Record to retain |
|---|---|---|
| Finish identity | Approved system and current part revision | Lot-linked finish and process identification |
| Cosmetic appearance | Surface zones, viewing instruction and references | Observed defects and cosmetic disposition |
| Functional features | Mask boundaries and finished interface requirements | Applicable gauge or assembly-check results |
| Coating performance | Agreed test plan and acceptance criteria | Applicable reports and specimen traceability |
| Repaired or deviated parts | Authorized scope and repeat-check requirements | Quantity, approval and final disposition |
Route uncertain findings to the named decision owner and preserve representative evidence. Use the structural-component inspection guide for the broader inspection structure and the packaging guide for the separate transport-protection discussion. The finish handoff is complete when both teams can reach and document the same acceptance decision using the issued requirements.
11. Sources and engineering boundaries
These primary references support the limited technical background identified inline. Public summaries establish scope, not a complete test procedure. Obtain the applicable controlled standards and coating-supplier instructions for actual work. The tables and dispute scenario are original planning aids; they supply no universal finish limits, KINGSUN test results or customer acceptance records.